Inspection before shipment is the last chance to find a non-conformance while the material is still at the mill or warehouse, where correction is possible. After the pipe is on the water, a dimensional or documentation problem becomes a claim, a delay or an argument. The inspection should follow an inspection and test plan and leave a document trail for every hold and witness point.
What the inspection should verify
- Identity Heat number, size, grade, specification and marking.
- Dimensions Outside diameter, wall thickness, length, straightness, end preparation and bevel.
- Surface Laminations, cracks, pitting, coating damage and foreign material.
- Weld Weld profile, repair evidence and non-destructive examination results where required.
- Tests Mechanical test results, impact results, hydrostatic test results and supplementary tests.
- Documents Mill test certificate, packing list, inspection reports and release note.
ITP: hold points and witness points
| Point | What it means | Buyer action |
|---|---|---|
| Hold point | Work cannot proceed until the buyer or inspector approves | Attend or delegate a nominated inspector and record the result |
| Witness point | The buyer may attend; work can proceed if no attendance is arranged | Decide in advance which points to attend |
| Review point | The document must be submitted for review | Check before the next production step |
The inspection and test plan should be agreed before production. Adding a witness point after testing has started may be impossible or may mean repeating a test.
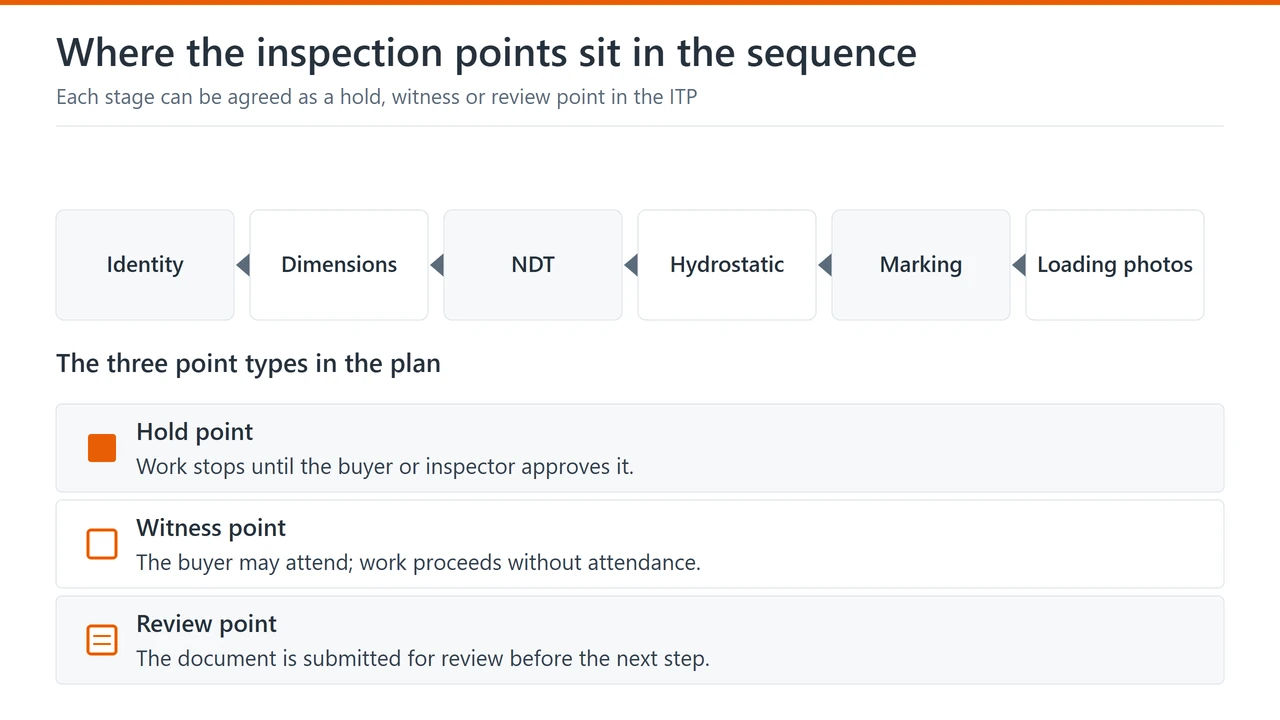
Dimensional, NDT and hydrostatic checks
Dimensional inspection is not a random glance. Check the outside diameter, wall thickness and length against the standard and the purchase order, and record the method and the instruments used. For welded pipe, confirm that the weld seam was examined by the non-destructive method required for the process. Hydrostatic test pressure, holding time and any pressure drop must be traceable to the test chart or record, not stated as “tested”.
Marking, packing and pre-load photos
Before the material is loaded, photograph the markings, the bundle tags, the end protectors, the coating condition and the stowage. The photographs should show enough context to identify the bundle later. Keep a copy of the packing list beside the photos. This is the evidence you will use if a bundle arrives wet, shifted, missing tags or damaged in transit.
Documents to keep
- ITP Approved inspection and test plan with witness and hold points marked.
- MTC EN 10204 3.1 or 3.2 certificate with heat traceability.
- Test reports NDT, hydrostatic, impact and any supplementary tests.
- Inspection release Signed release note before shipment.
- Photos Marking, packing, coating and loading condition.
Where to go next
- Boiler & Heat Exchanger Tube – product supply range
- EN 10204 3.1 vs 3.2 – certificate types and who signs
- Quality Control – inspection and testing scope
- Get a Quote – send the specification and destination port
Need a pre-shipment inspection arranged? Send the standard, grade, outside diameter, wall thickness, length and quantity, and we will reply with availability and pricing.
Request a quotation