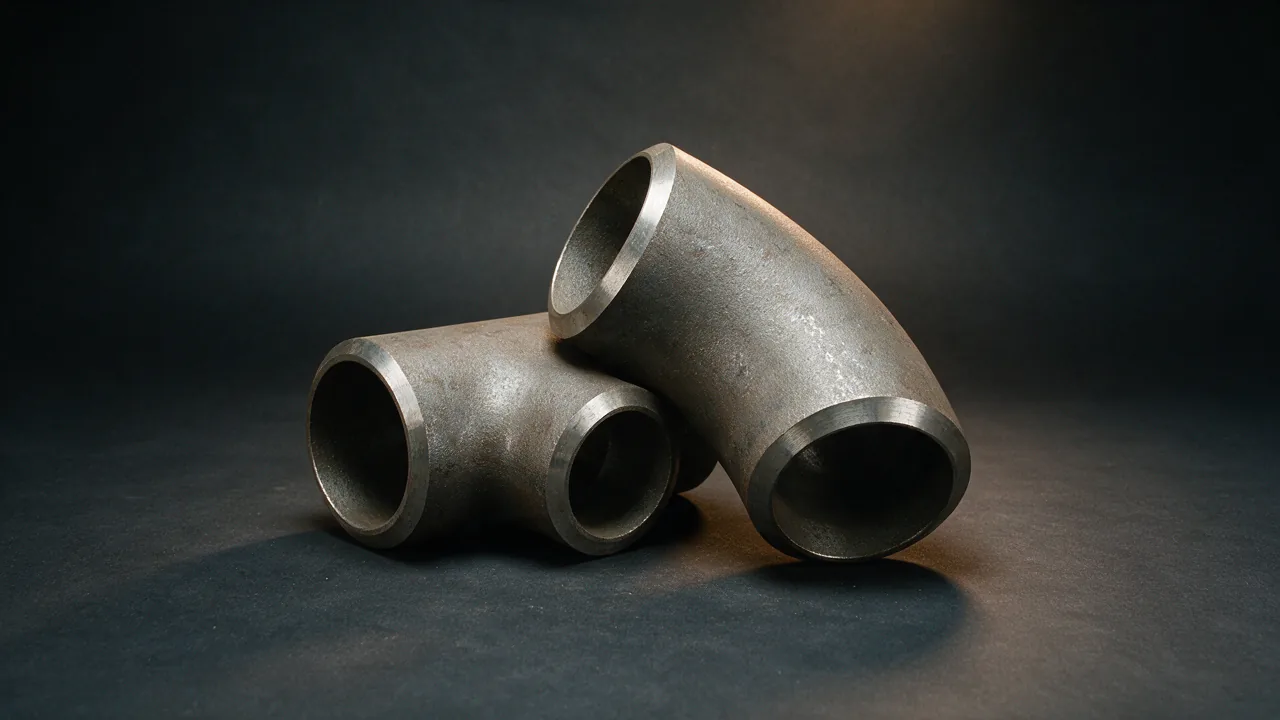
Chrome-moly alloy steel butt weld fittings to ASTM A234 in WP5, WP9, WP11, WP12, WP22 and WP91 for high temperature and hydrogen service.
- Standard: ASTM A234, ASME B16.9, ASME B16.25, ASTM A182, NACE MR0175
- Grades: WP5, WP9, WP11, WP12, WP22, WP91, WP92, F11, F22, F91
- Certificate: EN 10204 3.1 with every order, 3.2 on request
Mejor Steel is the export agent for the mills that make your material: one contract, one delivery date, and the mill named on the quotation. How we supply
We reply within one business day, Monday to Friday 09:00-18:00 CST. Or write to info@mejorsteel.com / WhatsApp.
Specifications
| Outer diameter | 1/2" - 48" (DN15 - DN1200) |
|---|---|
| Wall thickness | SCH 10 - XXS |
| Schedule | SCH 10 to XXS, heavy wall available |
| Length | Center to end per ASME B16.9 |
| Ends | Bevelled to ASME B16.25, or smooth finish |
| Surface treatment | Black, varnish, or protective coating |
| Manufacturing process | Seamless, forged and machined, or welded |
| Pressure rating | Per ASME B16.9 wall thickness and ASME B31.3 |
Reading the Chrome-Moly Grades
Chrome-moly grades are named by their chromium and molybdenum content, and the grade choice is driven by design temperature and by hydrogen partial pressure. WP11 is 1-1/4Cr-1/2Mo and is the most widely used grade, covering refinery piping up to about 550 degrees Celsius. WP22 is 2-1/4Cr-1Mo, with higher creep strength at elevated temperature and better resistance to hydrogen attack, used in hydrocracker and hydrotreater circuits. WP5 is 5Cr-1/2Mo and WP9 is 9Cr-1Mo, both used in higher temperature and more corrosive refinery service. WP91, which is 9Cr-1Mo-V, has substantially higher creep strength than WP22 and allows thinner walls at the same temperature and pressure, which is why it dominates modern high energy piping in power plants. The addition of vanadium and niobium in WP91 is what provides the improved creep performance, and it also makes the material more sensitive to welding heat input.
Why PMI Matters More Here
Alloy steel fittings look and weigh almost the same as carbon steel fittings, and a grade substitution between WP11 and carbon steel WPB, or between WP22 and WP11, would not be visible on the rack. The consequence, however, is serious: an incorrect grade in a high temperature hydrogen line can fail by hydrogen attack or by creep rupture at temperatures well below the design condition, and the failure can be catastrophic. For this reason, positive material identification is not optional on chrome-moly fittings. X-ray fluorescence or optical emission spectrometry is used to measure the chromium and molybdenum content of every fitting, and the readings are recorded on the mill certificate. Some specifications also require hardness testing and, for thick sections, full heat treatment records. When ordering alloy steel fittings, state the requirement for PMI explicitly, and confirm the acceptance criteria for the measured chemistry.
Alloy fittings: chrome content is the specification
Chrome-moly fittings are made to A234 and the WP number states the chrome and molybdenum content, exactly as it does for the pipe. Because the chemistry is what gives the fitting its high temperature and hydrogen resistance, positive material identification on the finished fitting is a normal requirement rather than an extra.
| Where the fitting sits | What it fixes in the specification | What to state on the enquiry |
|---|---|---|
| Steam or high temperature line | WP11 or WP22, to match the A335 pipe | the pipe grade and the design temperature |
| Hydrogen or hydroprocessing service | The chrome content is set by the hydrogen partial pressure | the partial pressure and the operating temperature |
| Refinery hydrocracker or reformer | WP9, WP91 or WP92 for the higher grades | the project specification |
| Sour service | Restricted hardness applies to the fitting as well as the pipe | NACE MR0175 |
| Verification requirement | PMI is the standard check on chrome and molybdenum content | whether PMI is required, and to which standard |
| Heavy wall or thick section | Forged and machined blanks are used at the larger sizes | the size and the wall |
| Field welding of P91 or P92 | Controlled heat treatment is mandatory after welding | whether post weld heat treatment is required |
| Impact requirement | Charpy testing where the design calls for it | the test temperature |
What is the difference between WP11, WP22 and WP91?
WP11 is 1-1/4Cr-1/2Mo, used for general refinery high temperature piping up to about 550 degrees Celsius. WP22 is 2-1/4Cr-1Mo with higher creep strength and better hydrogen resistance, used in hydroprocessing circuits. WP91 is 9Cr-1Mo-V with much higher creep strength, allowing thinner walls at the same condition, and is the standard for modern power plant high energy piping. The grade is selected from a design temperature and hydrogen partial pressure evaluation, not from preference.
Is PMI required on alloy steel fittings?
In practice, yes. Alloy steel and carbon steel fittings are visually indistinguishable, so without PMI there is no way to confirm that a WP11 fitting is not actually WPB, or that a WP22 is not actually WP11. In high temperature hydrogen service a wrong grade can fail by hydrogen attack or creep. We perform PMI on every alloy steel fitting and report the measured chemistry on the certificate.
Grades supplied
The grade fixes the minimum strength and the chemistry. Select a grade for its full composition and mechanical tables.
- WP5
- WP9
- WP11
- WP12
- WP22
- WP91
- WP92
- F11
- F22
- F91
Download Alloy Steel Fittings data sheet (PDF) One page: supply range, grades and key sizes, what to state on the enquiry, and the inspection documents that come with the order. The standard is the governing document.
Materials
- 1-1/4Cr-1/2Mo
- 2-1/4Cr-1Mo
- 5Cr-1/2Mo
- 9Cr-1Mo
- 9Cr-1Mo-V
Typical applications
- Refinery and hydrocracker piping
- Hydrogen and hydrodesulfurization units
- Power plant high temperature steam lines
- Petrochemical high temperature service
- Sour service in oil and gas
Inspection & testing
- PMI to verify chrome and moly content
- Dimensional inspection per ASME B16.9
- Radiographic or ultrasonic examination
- Hardness testing
- Charpy impact testing
- Third-party inspection (SGS, BV, TUV)
| Packaging | Sea-worthy export packing: wooden cases or pallets, tagged with size, grade and heat number; corrosion protection on request. |
|---|---|
| MOQ | By piece - mixed sizes accepted; no minimum on standard items. |
| Lead time | Stock items: 5-10 days. Made to order: 3-5 weeks after order confirmation. |
Payment: T/T 30% deposit with the balance before shipment; L/C at sight also accepted. Final terms are confirmed on the quotation.
How we supply: sourced through partner mills; the producing mill is named on the quotation. How we supply sets out who is accountable for the order.
Need this product? Send the size, grade, quantity and destination port and we will reply with availability and pricing.
Request a quotation