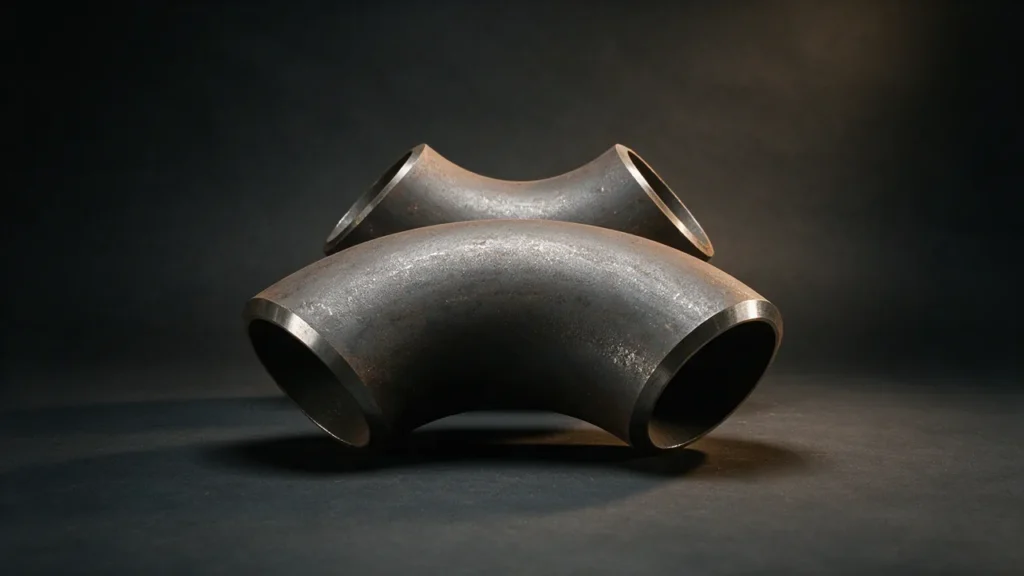
Mejor Steel is a China-based export agent for steel pipe fittings: butt weld to ASME B16.9, socket weld and threaded to ASME B16.11, and olets to MSS SP-97, in A234 WPB, A403 stainless and alloy steel. The mill that makes your fittings is named on the quotation, so the standard, the grade and the schedule travel with the order.
- Standards: ASTM A234 · ASME B16.9 · ASME B16.25 · ASTM A182 · NACE MR0175 · ASTM A403 · MSS SP-43 · MSS SP-75 · ASTM A420 · ASME B16.20
- 12 products in this line
- MOQ By piece, no minimum on standard items
- Lead time Stock 5–10 days · made to order 3–5 weeks
- Certificate EN 10204 3.1 with every order, 3.2 on request
- Reply Within one business day

How the connection decides the fitting, and which page carries it
The way a fitting attaches is the first decision, and it settles the standard, the size basis and who can make it. Butt weld fittings are welded end to end with the pipe and are dimensioned to ASME B16.9, so they match the pipe bore and wall directly. Socket weld and threaded fittings are made to ASME B16.11 and are used on small bore lines where welding in place is difficult or hot work is not permitted. The table below routes the enquiry to the page that carries the detail.
| Family | Standard | How it attaches | Where it is used | Page |
|---|---|---|---|---|
| Butt weld fittings | ASME B16.9 | Welded end to end with the pipe, dimensioned to the pipe bore and wall | Process, pipeline and utility lines of any size; the default where the line will be welded | Elbow / Tee / Reducer / Cap |
| Socket weld fittings | ASME B16.11 | The pipe sits in a socket and is fillet welded | Small bore lines where welding in place is difficult, or where the alignment has to be held | Socket weld fittings |
| Threaded fittings | ASME B16.11 | Screwed, with the thread form stated on the order | Small bore utility and instrument lines, and connections that have to be broken | Threaded fittings |
| Olets and branch connections | MSS SP-97 | Welded onto the run pipe to make a branch | Branches where a tee is not available or not wanted, and where the run must stay full bore | Olets |
| Hammer unions | Manufacturer standard | Wing nut and seat, made up by hand | Temporary and high pressure connections that are made and broken repeatedly | Hammer unions |
| Flanges and gaskets | ASME B16.5 / B16.47 | Bolted joint, with the facing and the gasket as separate decisions | Every bolted joint in the line, and the point where most leaks start | Flanges / Gaskets and bolting |
The material follows the pipe rather than the fitting’s convenience: A234 WPB with carbon steel, A234 WP11, WP22 or WP91 with alloy, and A403 with stainless. Duplex and super duplex are supplied where the project permits them, and the joint between two different materials is a design decision, not a stock decision.
Within the family: the type carries the rest of the decision
The family settles the standard and the size basis. The type settles the geometry, and the geometry is what a fittings enquiry most often leaves out, so it is stated rather than assumed.
| Type | Geometry to state | The decision it answers | Page |
|---|---|---|---|
| Butt weld elbow (ASME B16.9) | 90° or 45°; long radius (1.5 × NPS), short radius (1.0 × NPS) or 3D | Long radius is the default for lower pressure drop and lower turbulence; short radius is for tight space and accepts a higher pressure loss. | Butt weld elbow |
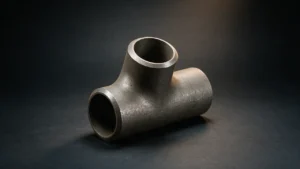
| Butt weld tee (ASME B16.9) | Equal or reducing | Equal where the line splits into two lines of the same size; reducing where a smaller line is tapped off the run. | Butt weld tee |
| Butt weld reducer (ASME B16.9) | Concentric or eccentric, and the flat side orientation if eccentric | Concentric holds a common centreline. Eccentric keeps either the top or the bottom of the line at a constant elevation, so the flat side orientation is a decision and not a default. | Butt weld reducer |
| Butt weld cap (ASME B16.9) | Cap or plug | A cap welds onto the outside of the pipe end and closes the line permanently. A plug goes inside a fitting and is made up on a thread or a socket. | Butt weld cap |
| Socket weld fittings (ASME B16.11) | Coupling, half coupling, elbow, tee or cross; class 3000, 6000 or 9000 | Small bore lines where the socket holds the alignment while the weld is made. | Socket weld fittings |
| Threaded fittings (ASME B16.11) | Coupling, elbow, tee, cap, plug or bushing; class 2000, 3000 or 6000 | Small bore utility and instrument lines, and connections that have to be broken. | Threaded fittings |
The class numbers in ASME B16.11 are not pressures in psi: class 3000 corresponds approximately to schedule 80 pipe, class 6000 to schedule 160, and class 9000 to XXS. The class is part of the fitting specification, not a preference.
What we supply: sizes and classes
The size and pressure class range for this line is below. Wall and material follow the pipe the fitting joins.
| Family | Size | Class or schedule |
|---|---|---|
| Butt weld fittings (B16.9) | 1/2–48 in (DN15–DN1200) | SCH 10–XXS, STD, XS |
| Socket weld fittings (B16.11) | 1/2–4 in (DN15–DN100) | 3000#, 6000#, 9000# |
| Threaded fittings (B16.11) | 1/8–4 in (DN6–DN100) | 2000#, 3000#, 6000# |
| Olets & branch connections (MSS SP-97) | run 1/2–48 in, branch 1/8–24 in | matches run pipe SCH 10–XXS |
| Hammer unions | 1–4 in (DN25–DN100) | 2000–20000 psi working, test to 30000 psi |
| Gaskets & bolting | for 1/2–60 in flanges | Class 150–2500 |
Common ASME B16.9 dimensions (mm)
Centre-to-end for a 90° long-radius elbow (A), and centre-to-end / centre-to-face for an equal tee (C = M). The full table to NPS 48 in is on ASME B16.9 fitting dimensions. Related: ASME B16.11 classes and sizes · MSS SP-97 olets.
Data sheets: Elbow · Tee · Reducer · Cap · Socket weld · Threaded (PDF)
| NPS | Pipe OD | 90° LR elbow A | Equal tee C = M |
|---|---|---|---|
| 1/2 | 21.3 | 38 | 25 |
| 3/4 | 26.7 | 38 | 29 |
| 1 | 33.4 | 38 | 38 |
| 1-1/4 | 42.2 | 48 | 48 |
| 1-1/2 | 48.3 | 57 | 57 |
| 2 | 60.3 | 76 | 64 |
| 2-1/2 | 73.0 | 95 | 76 |
| 3 | 88.9 | 114 | 86 |
| 4 | 114.3 | 152 | 105 |
| 5 | 141.3 | 190 | 124 |
| 6 | 168.3 | 229 | 143 |
| 8 | 219.1 | 305 | 178 |
| 10 | 273.0 | 381 | 216 |
| 12 | 323.8 | 457 | 254 |
How a fitting order is fixed
The order of the questions is the same as for pipe, and the first one is not the size.
- How the fitting attaches. Butt weld, socket weld or threaded — decided in the section above, because the attachment sets the standard and the size basis.
- The standard and the material. The standard follows the attachment and the material follows the pipe, both set out above. A fitting of the right shape and the wrong grade is still the wrong fitting.
- The size and the schedule. A butt weld fitting is dimensioned to match the pipe it joins, so the schedule matters: a fitting made for one wall will not line up with another. Where the two differ, the enquiry has to say so deliberately rather than leave the mill to guess.
- The pressure class. For a flanged joint, Class 150, 300, 600 and upwards set the wall and the bolting, and the facing and the gasket have to match the flange. For socket weld and threaded fittings, the ASME B16.11 class (3000, 6000 or 9000) is stated instead.
- Surface, finish and any coating. Pickled or bright annealed for stainless, galvanized or coated for carbon steel, and the coating is usually applied to the fitting as well as the pipe.
- Testing and documents. Which tests, and which certificate type – see the mill certificate guide.
To quote: fitting type, connection, standard and grade, size and schedule (or pressure class), quantity and destination port. Send them and we reply with availability and pricing within one business day. Send an enquiry or WhatsApp the specification.
Payment: T/T 30% deposit with the balance before shipment; L/C at sight. Delivery: FOB, CFR or CIF to your destination port. Inspection: third-party inspection (SGS, BV or TUV) on request. Fittings and the pipe they join are quoted on the same enquiry, so the schedule, wall and material match end to end.
Where fittings orders go wrong
| What goes wrong | Why it happens | What prevents it |
|---|---|---|
| The fitting does not line up with the pipe | The schedule was assumed rather than stated, and a butt weld fitting is dimensioned to the wall it was made for. | Put the pipe schedule on the fittings enquiry, and say it explicitly if the fitting is meant to differ. |
| Two standards confused at the same size | B16.9 and B16.11 fittings for the same nominal size are different parts with different end preparations, and the enquiry quoted only “fitting, 2 inch”. | Name the standard with the family, not just the size. |
| The material does not match the pipe grade | The fitting was ordered by shape and size, with the grade left to the mill’s stock. | Order the fitting grade alongside the pipe grade, and state whether a different grade at that joint is acceptable. |
| A branch with no allowance for the opening | An olet or a welded branch removes metal from the run pipe, and the reinforcement is decided by the design code rather than by the fitting. | Give the run size, the branch size and the design conditions, so the branch connection can be checked. |
| Coating applied before the fittings are made up | The coating sequence was set from the pipe, and the field joints end up with a different finish. | Agree the coating and the field joint treatment with the pipe order, not after it. |
Frequently asked questions
When is a socket weld fitting used instead of a butt weld fitting?
Socket weld fittings to ASME B16.11 are used on small bore lines, typically where there is not enough room to make a butt weld, where welding in place is difficult, or where the alignment has to be held by the socket while the weld is made. Butt weld fittings to B16.9 are the default for process and pipeline service because the joint is a full penetration weld that can be radiographed. The two are not interchangeable at the same nominal size: the end preparation and the dimensioning are different.
Do fittings have to match the pipe schedule?
For butt weld fittings, yes in practice: ASME B16.9 dimensioning is tied to the pipe it joins, and the wall at the end has to line up with the pipe wall for the weld to be sound. The schedule is therefore part of the fitting specification, not a property of the pipe alone. Where a fitting of a different wall is wanted deliberately, that is stated on the enquiry so it is priced and made as asked.
Which standard covers an olet?
MSS SP-97 is the standard for integrally reinforced forged branch outlet fittings. What the standard does not decide is whether the branch needs reinforcement: an opening in a run pipe is a design question answered by the piping code, using the run size, the branch size and the design conditions. That is why an olet enquiry needs the run and branch together rather than the branch alone.
Are you a manufacturer or an export agent?
Mejor Steel is a trading company and export agent based in Anyang, Henan; we do not own production equipment. The partner mill makes the fittings and issues the mill test certificate from its own laboratory, and the producing mill is named on the quotation before you place the order. The contract, the delivery schedule and any claim are handled by us.
What decides the price
There is no list price for fittings: the same drawing can be quoted at different numbers depending on seven things. Send them and the quotation comes back within one business day.
| Factor | Why it moves the price | What to send |
|---|---|---|
| Material grade | ASTM A234 WPB is the baseline; WP11, WP22, WP91, WP304/316 and duplex grades cost more and take longer to source | The grade, or the line class |
| Size and wall schedule | Weight and forming time rise with both; the schedule is part of the fitting, not an afterthought | NPS and schedule (SCH 40, 80, 160, XXS) |
| End preparation | A bevelled end to ASME B16.25, a socket or a thread are different machining operations | Butt weld, socket weld or threaded |
| Manufacturing route | A seamless fitting and a welded one are not the same cost at the same size | Seamless or welded, if the specification requires one |
| Quantity | Setup is spread over the pieces; a small lot carries more per piece | Pieces, or total weight |
| Inspection and certificate | Radiography, PMI, EN 10204 3.2 and third-party inspection add cost and time | 3.1 or 3.2, NDT and whether SGS, BV or TUV is required |
| Destination and Incoterm | Freight and packing follow the port | Destination port, FOB / CFR / CIF |
Reply within one business day. Send the seven items above with the quantity and the destination port. Send the specification or WhatsApp the specification.
Butt Weld Fittings7
 Alloy Steel FittingsASTM A234 · ASME B16.9Chrome-moly alloy steel butt weld fittings to ASTM A234 in WP5, WP9, WP11, WP12, WP22 and WP91 for high temperature and hydrogen…
- Butt Weld CapASME B16.9 · ASME B16.25Butt weld caps to ASME B16.9 in carbon steel, alloy steel and stainless steel, from 1/2 inch to 48 inch, for closing…
- Butt Weld ElbowASME B16.9 · ASME B16.25Long radius and short radius 90 degree, 45 degree and 180 degree butt weld elbows to ASME B16.9 in carbon steel, alloy…
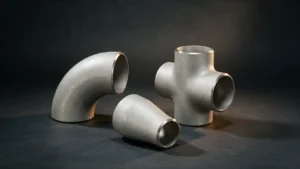
- Butt Weld FittingsASME B16.9 · ASME B16.25Butt weld elbows, tees, reducers, caps and stub ends to ASME B16.9 and ASTM A234 WPB, 1/2 to 48 inch, in carbon,…
- Butt Weld ReducerASME B16.9 · ASME B16.25Concentric and eccentric butt weld reducers to ASME B16.9 in carbon steel, alloy steel and stainless steel, from 1/2 inch to 48…
- Butt Weld TeeASME B16.9 · ASME B16.25Equal and reducing butt weld tees to ASME B16.9 in carbon steel, alloy steel and stainless steel, from 1/2 inch to 48…
- Stainless Steel Butt Weld FittingsASTM A403 · ASME B16.9Stainless steel butt weld elbows, tees, reducers and caps to ASTM A403 and ASME B16.9 in WP304, WP316, WP321, WP347 and duplex…

Olets & Branch Connections1
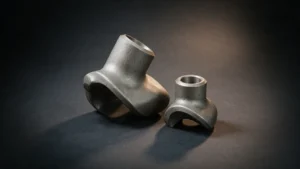
Socket Weld Fittings1
Pipe Fittings – grades, materials and ordering
| Grades | WP5 · WP9 · WP11 · WP12 · WP22 · WP91 · WP92 · F11 · F22 · F91 · WPB · WP304 · WP304L · WP316 · WP316L · WPC |
|---|---|
| Materials | 1-1/4Cr-1/2Mo · 2-1/4Cr-1Mo · 5Cr-1/2Mo · 9Cr-1Mo · 9Cr-1Mo-V · Carbon steel · Alloy steel · Stainless steel |
| Typical service |
|
| Minimum order | By piece - mixed sizes accepted; no minimum on standard items. |
| Lead time | Stock items: 5-10 days. Made to order: 3-5 weeks after order confirmation. |
| Packing | Sea-worthy export packing: wooden cases or pallets, tagged with size, grade and heat number; corrosion protection on request. |
How an order runs end to end — payment terms, inspection and release, packing and marking, and the documents that travel with the goods — is set out on how to order. Which standard applies to your service is covered under standards and grades; what is verified and tested on every order, and what the certificate says, under quality control. Which documents can travel with an order, and who issues each one, is listed under certifications and documents; who you would be buying from, and what we are accountable for on an order, is on about Mejor Steel.
Need a specific size, grade or quantity? Send the specification and the destination port and we will reply with availability and pricing.
Request a quotation