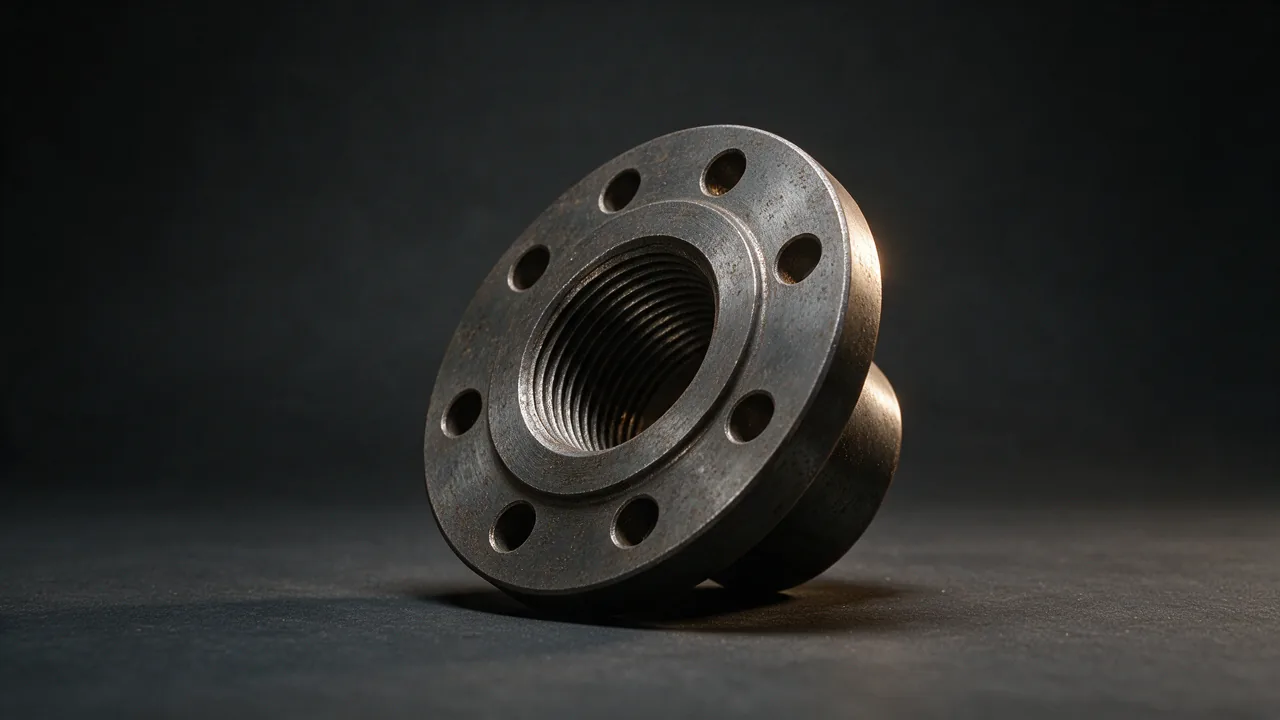
Small bore threaded flanges to ASME B16.5 with ASME B1.20.1 NPT threads, forged in carbon, alloy and stainless steel for lines where welding is not permitted.
- Standard: ASME B16.5, ASTM A105, ASTM A182, ASTM A350
- Grades: A105, A350 LF2, F11, F22, F304, F304L, F316, F316L
- Certificate: EN 10204 3.1 with every order, 3.2 on request
Mejor Steel is the export agent for the mills that make your material: one contract, one delivery date, and the mill named on the quotation. How we supply
We reply within one business day, Monday to Friday 09:00-18:00 CST. Or write to info@mejorsteel.com / WhatsApp.
Specifications
| Outer diameter | 1/2" - 4" to ASME B16.5 (highest classes up to 2 1/2") |
|---|---|
| Schedule | Threaded bore to suit the pipe thread - wall thickness series not required |
| Length | Flange thickness and thread depth per ASME B16.5 |
| Ends | Raised face (RF), flat face (FF) or ring joint (RTJ) |
| Surface treatment | Black oxide, anti-rust oil, hot dip galvanized, or machined finish |
| Manufacturing process | Forged and machined, threads cut and gauged |
| Pressure rating | Class 150, 300, 600, 900, 1500, 2500 |
| Connection type | Threaded to ASME B1.20.1 NPT - no welding |
ASME B16.5 Class 150 flange dimensions
Flange outside diameter, minimum flange thickness, bolt circle, bolting and raised face, in millimetres, for NPS 1/2 to 12 in. These dimensions are set by the size and the pressure class and are common to the flange types on this line; the bore, hub, socket or thread detail changes with the type and is confirmed on the drawing or the quotation. Thickness includes the 1.6 mm raised face.
| NPS | DN | Flange OD (mm) | Min. thickness (mm) | Bolt circle / PCD (mm) | Bolts | Bolt size | Hole dia (mm) | Raised face dia (mm) |
|---|---|---|---|---|---|---|---|---|
| 1/2 | 15 | 88.9 | 11.2 | 60.5 | 4 | M14 | 15.9 | 34.9 |
| 3/4 | 20 | 98.6 | 12.7 | 69.9 | 4 | M14 | 15.9 | 42.9 |
| 1 | 25 | 108.0 | 14.3 | 79.4 | 4 | M14 | 15.9 | 50.8 |
| 1-1/4 | 32 | 117.5 | 15.9 | 88.9 | 4 | M14 | 15.9 | 63.5 |
| 1-1/2 | 40 | 127.0 | 17.5 | 98.6 | 4 | M14 | 15.9 | 73.0 |
| 2 | 50 | 152.4 | 19.1 | 120.7 | 4 | M16 | 19.1 | 92.1 |
| 2-1/2 | 65 | 177.8 | 22.4 | 139.7 | 4 | M16 | 19.1 | 104.8 |
| 3 | 80 | 190.5 | 23.9 | 152.4 | 4 | M16 | 19.1 | 127.0 |
| 3-1/2 | 90 | 215.9 | 23.9 | 177.8 | 8 | M16 | 19.1 | 139.7 |
| 4 | 100 | 228.6 | 23.9 | 190.5 | 8 | M16 | 19.1 | 157.2 |
| 5 | 125 | 254.0 | 23.9 | 215.9 | 8 | M20 | 22.2 | 185.7 |
| 6 | 150 | 279.4 | 25.4 | 241.3 | 8 | M20 | 22.2 | 215.9 |
| 8 | 200 | 342.9 | 28.4 | 298.5 | 8 | M20 | 22.2 | 269.9 |
| 10 | 250 | 406.4 | 30.2 | 362.0 | 12 | M24 | 25.4 | 323.9 |
| 12 | 300 | 482.6 | 31.8 | 431.8 | 12 | M24 | 25.4 | 381.0 |
Data to ASME B16.5; confirm against the project specification before fabrication. Sizes above 12 in and Class 300 to 2500 follow the same layout and are quoted against the specification. Send the size, class, facing and destination port and we will confirm availability and price within one business day.
What a Threaded Flange Is
A threaded flange has a tapped bore instead of a plain or socketed one. The pipe is threaded and screwed into the flange, so the joint is made without any welding at all. In ASME B16.5 the thread is a tapered pipe thread to ASME B1.20.1 (NPT), which seals on the threads themselves with a sealant or tape; the pipe end is normally a standard pipe thread with a wrench-up of a few turns past hand-tight.
Why Choose Threaded Instead of Welded
The reason to choose a threaded connection is that there is no hot work. That matters when the connection has to be made on a plant that is already running, in a classified or hazardous area where a welding permit cannot be obtained, and on small bore connections where a weld would be difficult to fit. A threaded joint can also be unscrewed, which suits connections that have to come apart for cleaning, replacement of a gauge, or a temporary test point. The cost is a joint that is more prone to loosening and to leaking under vibration and thermal cycling, so it is rarely used above small bore sizes.
Size Range and Thread Specification
Threaded flanges are a small bore product: ASME B16.5 tabulates them up to NPS 4, and the highest classes stop at NPS 2 1/2. The thread type must be stated on the order, because NPT and other thread forms are not interchangeable – an NPT flange will not seal on a parallel thread pipe end. Threads are gauged before dispatch and the threaded bore is capped for shipment so that the thread arrives undamaged.
Limitations to Know
Do not use a threaded joint where the service is subject to severe vibration or thermal cycling, or where a leak cannot be tolerated – a threaded connection is the most likely of the small bore joints to work loose. It is also not suitable for very high pressure or for services where the fluid attacks the thread sealant. Where a welded joint is acceptable, a socket weld flange gives a stronger and more leak-tight small bore connection.
What thread standard do your threaded flanges use?
ASME B16.5 threaded flanges are tapped to ASME B1.20.1 NPT, which is the tapered pipe thread used with NPT pipe ends and fittings. The thread type is confirmed at the order stage because the flanges must match the pipe end they will be screwed onto.
When should I use a threaded flange instead of a socket weld flange?
Use threaded where welding is not possible or not permitted: on a live plant, in a hazardous area without a hot work permit, or where the joint has to be taken apart later. Use socket weld where welding is acceptable, because the welded joint is stronger and less likely to leak or loosen under vibration.
Can a threaded flange be used at high pressure?
It is not the preferred joint for high pressure or severe cyclic service. A threaded joint seals on the threads, which makes it more sensitive to vibration and thermal cycling than a welded joint. Above small bore sizes and high classes, butt welded connections are the normal choice.
How is the thread protected during shipment?
Threaded bores are fitted with plastic caps and the flanges are crated or palleted; the thread is gauged before dispatch so that any damage in transit is visible before installation rather than after.
NPT, BSPT and BSPP: which thread seals and which does not
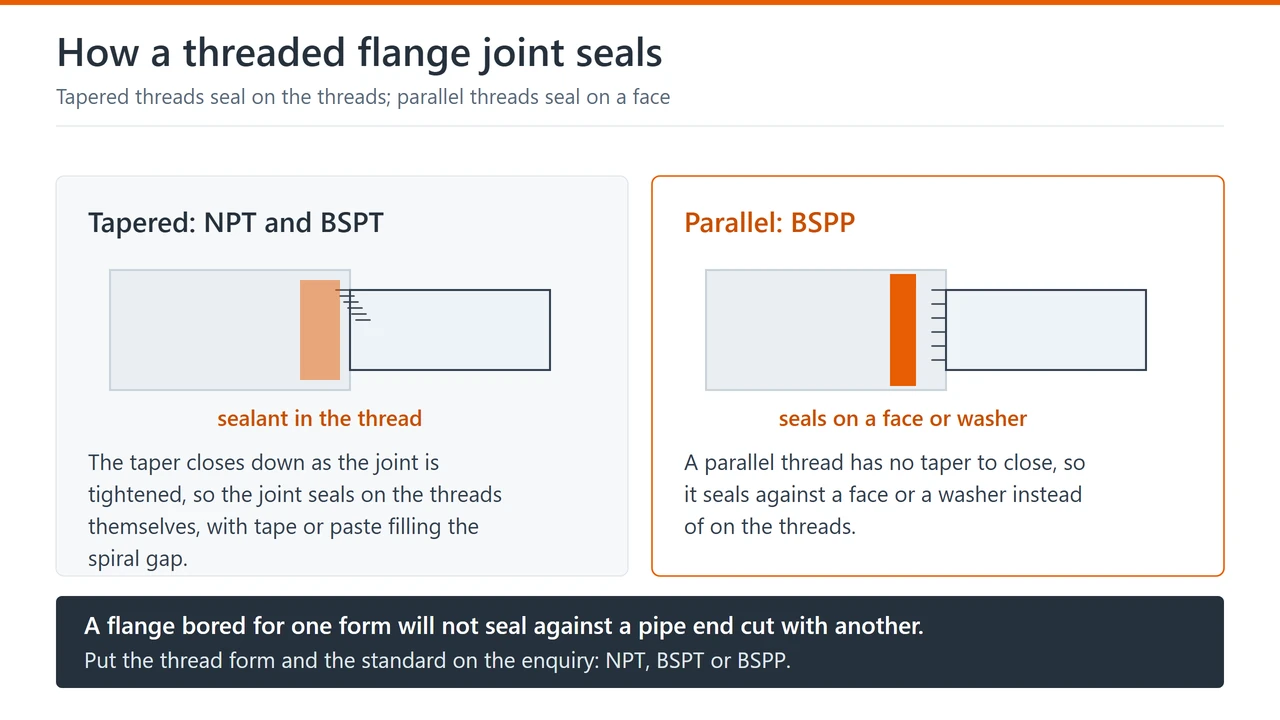
The B16.5 threaded flange is tapped with a tapered pipe thread. Tapered threads seal on the threads themselves; parallel threads seal on a face or a washer. A flange bored for one form will not seal against a pipe end cut with another, so the thread form has to be on the enquiry rather than assumed.
| Thread form | Standard | How the joint seals | What it means at the flange |
|---|---|---|---|
| NPT, tapered | ASME B1.20.1 | On the threads, with a sealant or tape as the joint is tightened | The default for a B16.5 threaded flange, and the form the matching pipe end is normally cut to |
| BSPT, tapered | ISO 7-1 / EN 10226-1 | On the threads, as with NPT | Similar taper but a different thread form; it will not seal against an NPT end |
| BSPP, parallel | ISO 228-1 | On a face or an elastomer seal, not on the threads | Needs a sealing washer or a matching face; a parallel end will not seal in a tapered bore |
| Other forms | Project or industry specific | Depends on the form | Confirm the form and the gauge before ordering |
Engagement, sealant and re-making the joint
- Engagement. A tapered thread is run up hand tight and then tightened a few turns past hand tight. Under tightening leaks; over tightening splits the flange boss or the fitting.
- Sealant. Tape or paste fills the spiral gap in the thread. Keep the first two threads clean so no tape ends up inside the line, and check that the sealant is compatible with the fluid.
- Re-making. A threaded joint can be broken and remade, which is the reason the type is chosen on a live plant, but each re-make takes the thread a little looser. Threads should be inspected and, where required, re-gauged before the joint is remade.
- Support. A threaded joint does not tolerate vibration or thermal cycling as well as a welded one, so lines that see either should be checked against the piping specification before threaded connections are used.
Grades supplied and minimum properties
The grade fixes the minimum strength and the chemistry. The table below gives the requirements that separate the forged flange material grades ordered most often; the full composition and mechanical table for each grade is on its own page.
| Grade | Yield strength | Tensile strength |
|---|---|---|
| A105 (forged carbon steel) | 250 MPa (36,000 psi) | 485 MPa (70,000 psi) |
| F316 (forged stainless steel) | 205 MPa min (30,000 psi) | 515 MPa min (75,000 psi) |
The complete chemistry and mechanical table for each grade, with the notes that qualify it, is on the individual grade page – for example ASTM A105 flange. The stainless grade has the higher tensile requirement but the lower minimum yield strength, so the two are not interchangeable on the strength table alone. The pressure class sets the flange dimensions, so the grade does not set the wall.
Source: specified minimum yield and tensile strength for each grade, per ASTM A105 / ASME SA105 and ASTM A182 / ASME SA182. The standard named against each grade is the governing document.
Download Threaded Flange data sheet (PDF) One page: supply range, grades and key sizes, what to state on the enquiry, and the inspection documents that come with the order. The standard is the governing document.
What decides the price
There is no list price for flanges: the same drawing can be quoted at different numbers depending on seven things. Send them and the quotation comes back within one business day.
| Factor | Why it moves the price | What to send |
|---|---|---|
| Material grade | Carbon A105 is the baseline; F316, F51 and alloy grades cost more and take longer to source | The grade, or the line class |
| Size and pressure class | Weight and forging time rise with both | NPS and class |
| Facing | RTJ and special facings add machining | RF, FF or RTJ |
| Bore or schedule | A weld neck is bored to the pipe wall, so the schedule is part of the price | The pipe schedule |
| Quantity | Setup is spread over the pieces; a small lot carries more per piece | Pieces, or total weight |
| Inspection and certificate | EN 10204 3.2 and third-party inspection add cost and time | 3.1 or 3.2, and whether SGS, BV or TUV is required |
| Destination and Incoterm | Freight and packing follow the port | Destination port, FOB / CFR / CIF |
Reply within one business day. Send the seven items above with the quantity and the destination port. Send the specification or WhatsApp the specification.
Materials
- Forged carbon steel
- Forged alloy steel (Cr-Mo)
- Forged stainless steel
Typical applications
- Tie-ins and tie-in points on live plant
- Areas where hot work is not permitted
- Instrument, gauge and sampling connections
- Small bore utility, drain and vent lines
- Connections that may have to be dismantled
- Oil and gas plant instrument and utility connections
Inspection & testing
- Dimensional inspection per ASME B16.5
- Thread gauging to ASME B1.20.1
- Chemical and mechanical testing per ASTM
- PMI on alloy and stainless steel
- Hardness testing
| Packaging | Sea-worthy export packing: wooden cases or pallets, tagged with size, grade and heat number; corrosion protection on request. |
|---|---|
| MOQ | By piece - mixed sizes accepted; no minimum on standard items. |
| Lead time | Stock items: 5-10 days. Made to order: 3-5 weeks after order confirmation. |
Payment: T/T 30% deposit with the balance before shipment; L/C at sight also accepted. Final terms are confirmed on the quotation.
How we supply: sourced through partner mills; the producing mill is named on the quotation. How we supply sets out who is accountable for the order.
Need this product? Send the size, grade, quantity and destination port and we will reply with availability and pricing.
Request a quotation