Electric resistance welded line pipe to API 5L PSL1 and PSL2, grades B to X70. Cost-effective thin-wall option for low to medium pressure lines from NPS 1/2 inch to 24 inch.
Pipe types: Seamless · ERW · LSAW · SSAW
- Standard: API 5L, ISO 3183, ASTM A53, ASME B36.10
- Grades: Grade B, X42, X46, X52, X56, X60, X65, X70
- Certificate: EN 10204 3.1 with every order, 3.2 on request
Mejor Steel is the export agent for the mills that make your material: one contract, one delivery date, and the mill named on the quotation. How we supply
We reply within one business day, Monday to Friday 09:00-18:00 CST. Or write to info@mejorsteel.com / WhatsApp.
Specifications
| Outer diameter | 1/2" - 24" (12.7 - 610 mm) |
|---|---|
| Wall thickness | SCH 10 - SCH 80, or 2.0 - 25.4 mm |
| Schedule | SCH 10, 20, 40, 80, or custom |
| Length | 6 m, 12 m, 20 FT, 40 FT, or custom 5 - 18 m |
| Ends | Plain, beveled, threaded |
| Surface treatment | Black painting, varnish, 3PE/3LPE, FBE, galvanized |
| Manufacturing process | Electric resistance welding (high frequency) |
| Pressure rating | Low to medium pressure service |
How ERW Pipe Is Made
ERW stands for electric resistance welding. A steel coil is unrolled, formed into a cylindrical shape through a series of rollers, and the two edges are pressed together while a high frequency alternating current is passed through them. The resistance at the faying surfaces generates enough heat to bring the steel to welding temperature, and the pressure roll forges the edges into a solid, forged weld. No filler metal is used. The external weld flash is then scarfed off, and the internal flash is either left in place or removed depending on the specification. Because the process starts from coil, ERW pipe is produced continuously at high speed, which is why it is significantly cheaper per ton than seamless pipe in the same size range.
When to Choose ERW Instead of Seamless
ERW pipe is the economical choice for low to medium pressure service in sizes up to 24 inch where the wall thickness is relatively thin. It is widely used for water lines, gathering lines, structural and piling work, and fire protection systems. The limitation is the weld seam: it is the area most vulnerable to preferential corrosion and to failure under cyclic loading, which is why ERW pipe is generally not accepted for high pressure transmission lines, sour service, or critical offshore applications. As a rule of thumb, if the wall thickness exceeds about 12 mm, or if the line will operate above roughly 60 percent of the specified minimum yield strength, seamless or LSAW pipe is the safer choice.
Where ERW pipe is the right answer, and where it is not
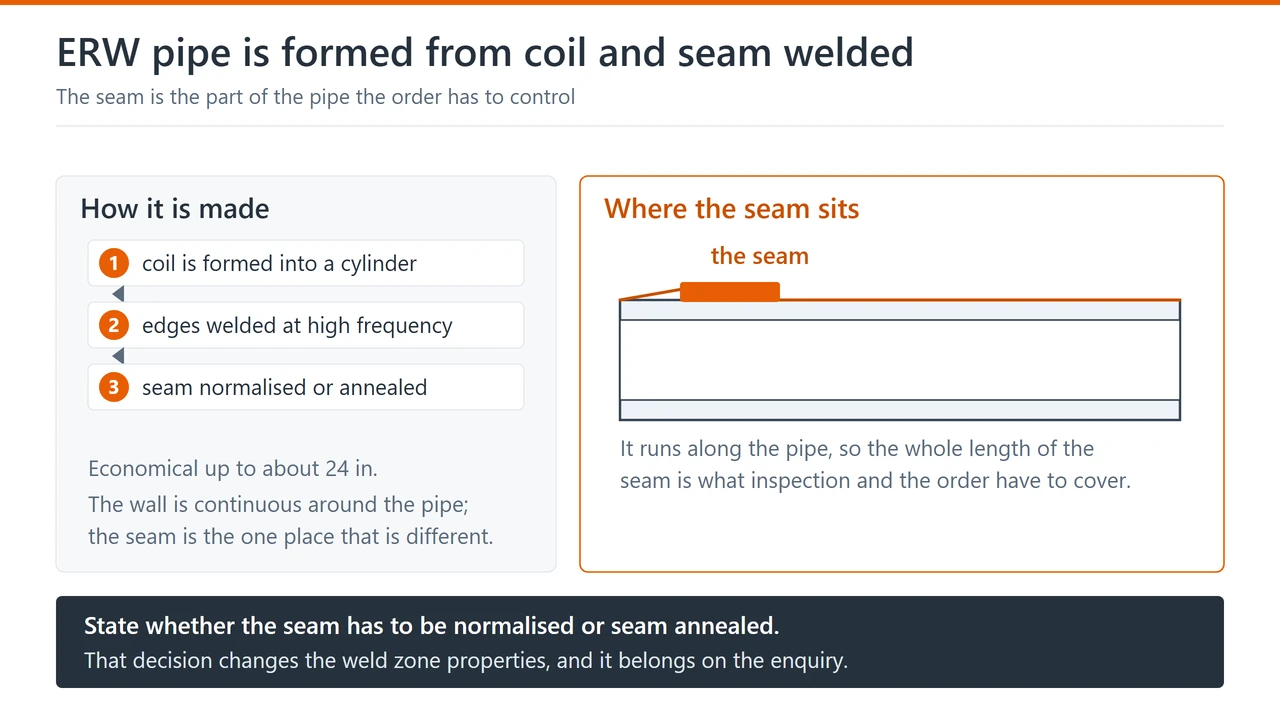
ERW pipe is formed from coil and seam welded at high frequency, which makes it the most economical way to produce pipe up to about 24 in. The weld seam is the part that has to be controlled, so the question is not only what the pipe carries but how much inspection that seam is going to get.
| Service condition | What it decides | What to state on the enquiry |
|---|---|---|
| Low to medium pressure water or utility line | The ERW wall is adequate and cost per metre is the real driver | the design pressure, so the wall can be set from it |
| Oil and gas gathering line | Seam quality matters more than diameter at this size | whether full length seam inspection is required |
| Structural, piling or scaffolding use | No pressure rating is involved at all | state ‘structural’ and the length, so pressure testing is not quoted twice |
| Galvanized or coated finish | The coating goes on after welding, so the seam is not exposed by it | the coating type, and whether cut ends have to be coated |
| High integrity or cyclic service | ERW is often ruled out in favour of seamless or LSAW | state the restriction early so the alternative can be offered |
Is ERW pipe as strong as seamless pipe?
For the same grade and wall thickness, ERW and seamless pipe have the same specified minimum yield and tensile strength, so the base material strength is equal. The difference is the weld seam. An ERW seam is a forged weld that in well-controlled production achieves full parent-metal strength, but it remains a discontinuity. This is why standards restrict ERW pipe for certain critical services and why full-length seam inspection is mandatory. For water, gathering and structural service the difference is not significant; for high pressure or sour service it is.
What does the ERW pipe price difference look like compared with seamless?
As a general market indication, ERW pipe is typically 5 to 15 percent cheaper per ton than seamless pipe in the same grade and comparable wall thickness, with the gap widening for thin-wall sizes and narrowing as wall thickness increases. The actual differential moves with coil and billet prices, so a current quotation should always be requested for a specific specification.
The weld seam is what the order has to control
An ERW seam is made by heating the strip edges and forging them together, without filler metal. In controlled production the seam reaches parent metal strength, and the specification tests its strength on the sample. The defects that matter in service are the ones a strength test does not always find:
| Defect | What it is | How it is screened |
|---|---|---|
| Cold weld | The edges joined without reaching forging temperature, so the bond is incomplete | Ultrasonic testing of the seam; a cold weld can pass a flattening test on a short sample |
| Penetrator or hook crack | Oxide or a folded edge trapped in the seam | Ultrasonic testing, and visual inspection of the seam inside and outside |
| Stitching | Short unwelded sections along the seam | Continuous non destructive inspection rather than spot checks |
That is why the enquiry should name the inspection, and not only the grade. Visual inspection alone does not find a cold weld, and a random sample does not find stitching.
What to write on an ERW order
- Specification and level: API 5L PSL1 or PSL2, or ASTM A53 / A106 where the project allows welded pipe. A106 does not permit welded construction, so a welded pipe cannot be certified to it.
- Non destructive inspection of the seam: ultrasonic testing, eddy current testing, or the mill’s standard inspection where the project has not named one.
- Hydrostatic test: each length is tested, with the pressure and hold time from the specification or the purchase order.
- Weld seam condition: whether the seam has to be normalised or seam annealed after welding, which affects the weld zone properties.
- Seam marking and orientation: whether the weld line is marked, and whether the seam has to be positioned away from the bending plane where the pipe will be bent in the field.
- Certification: mill test certificate, and whether the project asks for EN 10204 3.2 or third party inspection.
The inspection method, test pressure and seam treatment are taken from the specification and the purchase order. Where the project has not named a method, we confirm the mill’s standard scope in writing before the order is released.
ERW, seamless or SSAW: what changes in the order
The three processes give the same specified minimum strength for the same grade, so the difference at the order stage is not strength. It is the seam, the inspection that follows from it, and the price order that results.
| Process | Practical range | Inspection that comes with the order | Relative price | Where it is the wrong answer |
|---|---|---|---|---|
| ERW | Small to medium diameter, thinner wall, up to about 24 in | Weld seam non destructive inspection, plus hydrostatic test on every length | Lowest of the three in the same grade | High pressure gas transmission where the specification calls for seamless or LSAW |
| Seamless | Small to medium diameter in heavier wall, and larger sizes on request | No seam inspection needed, so hydrostatic and mechanical testing dominate | Highest of the three | Thin wall, large diameter work where the coil based process is far cheaper |
| SSAW | Large diameter, one line covering a wide range | Weld seam inspection on a much longer helical seam, with the method agreed in advance | Between ERW and seamless at large diameter | High pressure gas lines unless the project permits spiral welded pipe |
The price relationship is directional, not a quotation: ERW sits below seamless in the same grade, and the gap narrows as wall thickness increases. The percentage band we publish for ERW against seamless is on this page in the price question above, and the actual figure is confirmed per enquiry because it moves with coil and billet prices.
What the buyer pays for in the difference is the inspection: an ERW order carries weld seam inspection and its cost and lead time, a seamless order does not need it but carries a higher price at the mill. On large diameter work the same reasoning applies to the helical seam of SSAW, where the seam is longer and the inspection scope has to be agreed before production rather than after.
A short checklist before the process is fixed
- What does the line carry, and what does the project specification permit: seamless, ERW, LSAW or SSAW?
- Which non destructive inspection does the specification require on the seam, and who witnesses it?
- Is the wall thickness fixed, or is it still open, because the process choice follows the wall as much as the pressure?
- What is more expensive for this project: a higher mill price for seamless, or inspection and lead time on a welded seam?
Process availability, inspection scope and price band are confirmed per enquiry. Where the project specification names a process, that specification decides; this page explains the trade off behind it.
Grades supplied and minimum properties
The grade fixes the minimum strength and the chemistry. The table below gives the requirements that separate the API 5L grades ordered most often; the full composition and mechanical table for each grade is on its own page.
| Grade | Yield strength | Tensile strength |
|---|---|---|
| Grade B | 245 MPa min (35,500 psi) | 415 MPa min (60,200 psi) |
| X42 | 290 MPa min (42,000 psi) | 414 MPa min (60,000 psi) |
| X52 | 359 MPa min (52,000 psi) | 455 MPa min (66,000 psi) |
| X60 | 414 MPa min (60,000 psi) | 517 MPa min (75,000 psi) |
| X65 | 448 MPa min (65,000 psi) | 531 MPa min (77,000 psi) |
| X70 | 483 MPa min (70,000 psi) | 565 MPa min (82,000 psi) |
| X80 | 555 – 705 MPa (80,500 – 102,300 psi) | 625 – 825 MPa (90,600 – 119,700 psi) |
The complete chemistry and mechanical table for each grade, with the notes that qualify it, is on the individual grade page – for example API 5L X65 PSL2 pipe. The grade fixes the strength; the weld is a separate qualification, and ERW pipe is normally supplied to the same grade requirements as seamless.
Source: specified minimum yield and tensile strength for each grade, per API 5L / ISO 3183, Table 7. The standard is the governing document.
Download API 5L ERW Welded Steel Pipe data sheet (PDF) One page: supply range, grades and key sizes, what to state on the enquiry, and the inspection documents that come with the order. The standard is the governing document.
Where to go next
- ERW vs HFW pipe – whether the two names describe one weld process, and what the order has to state.
- X65 and X70 line pipe – what the grade changes, and what it does not.
Materials
- Carbon steel
Typical applications
- Low and medium pressure water lines
- Oil and gas gathering lines
- Structural and piling applications
- Fence posts and scaffolding
- Fire protection piping
Inspection & testing
- Eddy current testing of the weld seam (full length)
- Ultrasonic testing of weld seam
- Hydrostatic pressure test
- Flattening and bend test
- Chemical and mechanical testing
- Third-party inspection (SGS, BV, TUV)
| Packaging | Sea-worthy export packing: bundled by size, plastic caps on both ends, corrosion protection on request, stencilled with size, grade and heat number. |
|---|---|
| MOQ | One bundle or one truckload; mixed sizes within a bundle accepted. |
| Lead time | Stock sizes: 7-15 days. Mill run / non-stock: 4-6 weeks after order confirmation. |
Payment: T/T 30% deposit with the balance before shipment; L/C at sight also accepted. Final terms are confirmed on the quotation.
How we supply: sourced through partner mills; the producing mill is named on the quotation. How we supply sets out who is accountable for the order.
Need this product? Send the size, grade, quantity and destination port and we will reply with availability and pricing.
Request a quotation