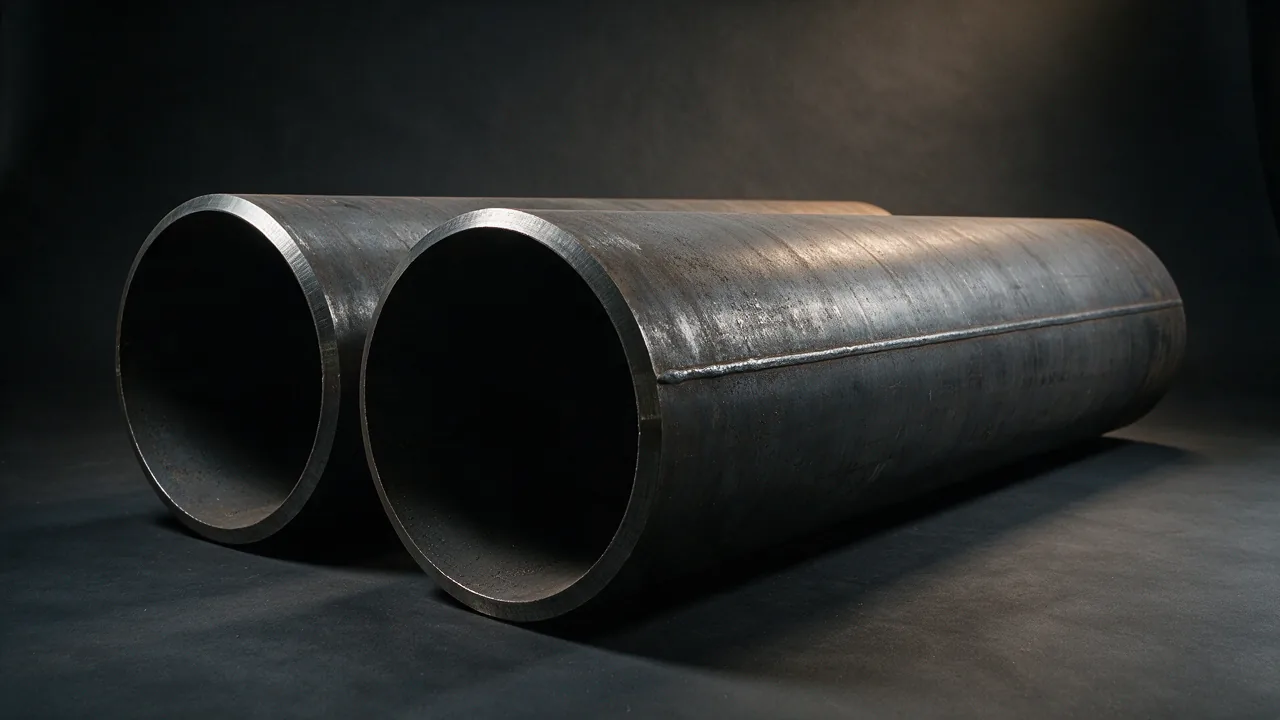
Longitudinally submerged arc welded line pipe to API 5L, grades B to X80, from 16 inch to 60 inch. The standard choice for large diameter, high pressure transmission mains.
Pipe types: Seamless · ERW · LSAW · SSAW
- Standard: API 5L, ISO 3183, ASME B36.10
- Grades: Grade B, X42, X52, X60, X65, X70, X80
- Certificate: EN 10204 3.1 with every order, 3.2 on request
Mejor Steel is the export agent for the mills that make your material: one contract, one delivery date, and the mill named on the quotation. How we supply
We reply within one business day, Monday to Friday 09:00-18:00 CST. Or write to info@mejorsteel.com / WhatsApp.
Specifications
| Outer diameter | 16" - 60" (406 - 1524 mm) |
|---|---|
| Wall thickness | 6 - 50 mm |
| Length | 6 m, 12 m, or custom up to 18 m |
| Ends | Beveled end, plain end |
| Surface treatment | Black painting, 3PE/3LPE, FBE, 3PP, concrete weight coating |
| Manufacturing process | Longitudinal submerged arc welding, JCOE or UOE forming |
| Pressure rating | High pressure transmission service |
What LSAW Pipe Is and Where It Is Used
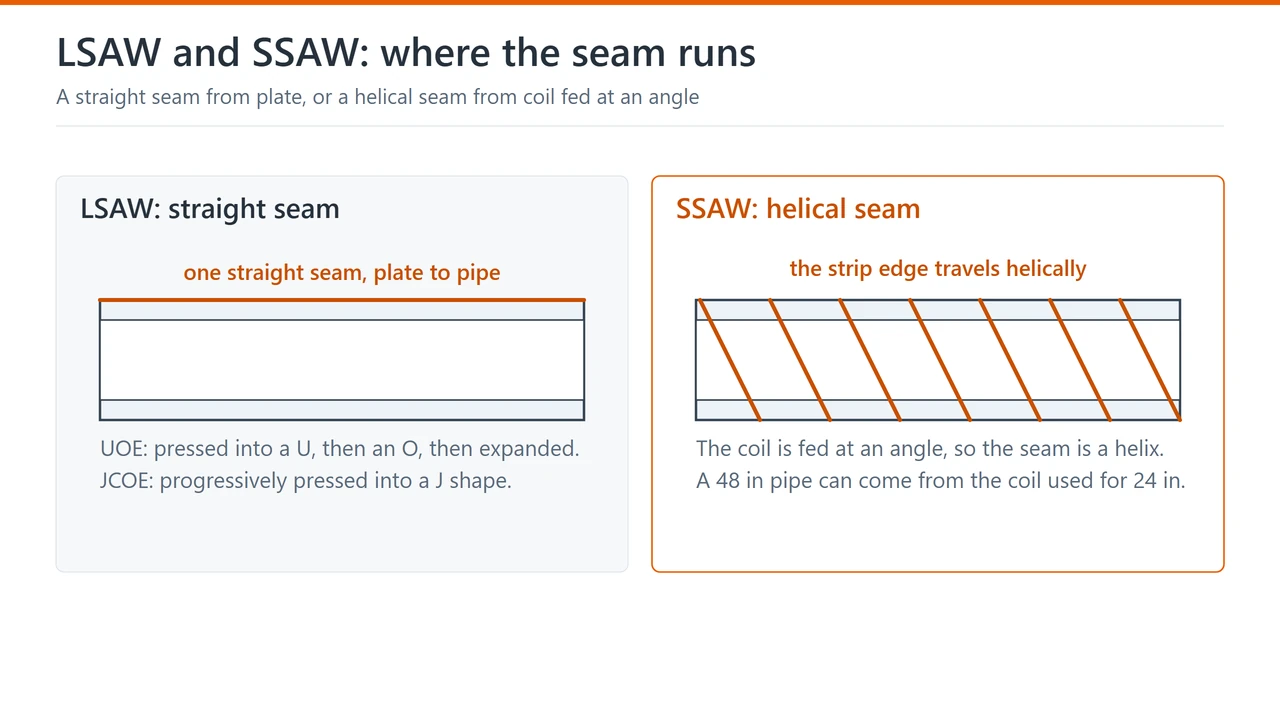
LSAW stands for longitudinal submerged arc welding. Steel plate is formed into a cylinder and the longitudinal seam is welded from both sides using the submerged arc process, in which the arc is buried under a layer of granular flux. This shields the weld from the atmosphere and produces a clean, ductile weld with excellent toughness. Because the process starts from plate rather than coil, wall thickness is not limited by coil gauge, which is why LSAW pipe is the normal choice for large diameter, heavy wall, high pressure transmission mains from 16 inch up to 60 inch. Two forming routes are common: UOE, where the plate is pressed into a U then an O shape and finally expanded, and JCOE, where the plate is progressively pressed into a J shape. Both produce pipe with excellent dimensional consistency.
LSAW vs SSAW – Choosing the Right Welded Pipe
SSAW (spiral submerged arc welded) pipe is made from coil wound at an angle, producing a helical seam. It is cheaper to produce in very large diameters and is excellent for lower pressure water and slurry lines. LSAW pipe has a straight longitudinal seam that runs parallel to the pipe axis. The practical difference is in the stress field: in an LSAW pipe the seam is oriented in the same direction as the principal hoop stress, but the weld is short and can be fully inspected; in an SSAW pipe the helical seam is longer and crosses the hoop stress direction, and the weld length per metre of pipe is roughly 1.5 to 2 times greater. For high pressure gas transmission where fracture control matters, LSAW is generally preferred. For large diameter, moderate pressure water mains, SSAW is usually more economical.
LSAW: the large diameter route for transmission pressure
LSAW pipe is formed from plate and welded along its length, which is how diameters from 16 in to 60 in are produced with a wall thick enough for transmission pressure. It is the grade and the wall that decide what the line can carry; the diameter only decides which mill can make it.
| Service condition | What it decides | What to state on the enquiry |
|---|---|---|
| Long distance transmission main | LSAW in PSL2 with impact testing, and a higher grade if the wall has to come down | grade, OD, wall, and the design factor the line is calculated to |
| City gas distribution at lower pressure | LSAW is still used for the diameter, but PSL1 may be sufficient | PSL level, and whether impact testing is required |
| Offshore or coastal pipeline | Tighter dimensional tolerance and full body inspection | the inspection scope, and whether concrete weight coating is needed |
| High pressure water main | The grade is usually modest; the coating and lining decide the service life | the internal lining and the external coating system |
| Many girth welds on site | Chemistry has to suit the welding procedure, not just the design | whether the welding procedure is already fixed by the contractor |
| Rock, urban or road crossings | Minimum wall may be set by handling and installation rather than by pressure | the minimum wall, and whether a heavier wall is specified |
What is the maximum diameter of LSAW pipe you can supply?
LSAW pipe is routinely supplied up to 48 inch outside diameter, and up to 60 inch for larger projects subject to mill availability. Wall thickness typically ranges from 6 mm to 50 mm. Above 60 inch, spiral welded (SSAW) pipe is generally the only practical option.
Do you provide charpy impact testing on LSAW pipe?
Yes. Charpy V-notch impact testing on the weld seam, heat affected zone and parent metal is standard for PSL2 pipe and can be provided on PSL1 pipe when specified. Test temperature can be set to the project requirement, for example 0 degrees C, minus 20 degrees C or minus 45 degrees C, with minimum absorbed energy typically specified as 27 J or 40 J average.
Grades supplied and minimum properties
The grade fixes the minimum strength and the chemistry. The table below gives the requirements that separate the API 5L grades ordered most often; the full composition and mechanical table for each grade is on its own page.
| Grade | Yield strength | Tensile strength |
|---|---|---|
| Grade B | 245 MPa min (35,500 psi) | 415 MPa min (60,200 psi) |
| X42 | 290 MPa min (42,000 psi) | 414 MPa min (60,000 psi) |
| X52 | 359 MPa min (52,000 psi) | 455 MPa min (66,000 psi) |
| X60 | 414 MPa min (60,000 psi) | 517 MPa min (75,000 psi) |
| X65 | 448 MPa min (65,000 psi) | 531 MPa min (77,000 psi) |
| X70 | 483 MPa min (70,000 psi) | 565 MPa min (82,000 psi) |
| X80 | 555 – 705 MPa (80,500 – 102,300 psi) | 625 – 825 MPa (90,600 – 119,700 psi) |
The complete chemistry and mechanical table for each grade, with the notes that qualify it, is on the individual grade page – for example API 5L X70 pipe. Higher grades are the usual choice on large diameter lines because they allow a thinner wall for the same design pressure.
Source: specified minimum yield and tensile strength for each grade, per API 5L / ISO 3183, Table 7. The standard is the governing document.
Download API 5L LSAW Welded Steel Pipe data sheet (PDF) One page: supply range, grades and key sizes, what to state on the enquiry, and the inspection documents that come with the order. The standard is the governing document.
Materials
- Carbon steel
Typical applications
- Long distance oil and gas transmission mains
- High pressure water transmission
- City gas distribution mains
- Offshore and coastal pipelines
- Power plant circulating water lines
Inspection & testing
- 100% ultrasonic testing of weld seam
- Radiographic testing (RT) on seam
- Hydrostatic pressure test
- Charpy V-notch impact test
- Full body ultrasonic inspection on request
- Third-party inspection (SGS, BV, TUV)
| Packaging | Sea-worthy export packing: bundled by size, plastic caps on both ends, corrosion protection on request, stencilled with size, grade and heat number. |
|---|---|
| MOQ | One bundle or one truckload; mixed sizes within a bundle accepted. |
| Lead time | Stock sizes: 7-15 days. Mill run / non-stock: 4-6 weeks after order confirmation. |
Payment: T/T 30% deposit with the balance before shipment; L/C at sight also accepted. Final terms are confirmed on the quotation.
How we supply: sourced through partner mills; the producing mill is named on the quotation. How we supply sets out who is accountable for the order.
Need this product? Send the size, grade, quantity and destination port and we will reply with availability and pricing.
Request a quotation